Custom Metal Fabrication Services
From raw tube and sheet to finished, zinc-plated assemblies — laser cutting, robotic welding, bending, stamping and CNC machining, all in our own 20-year-old workshop.
Send Your Drawing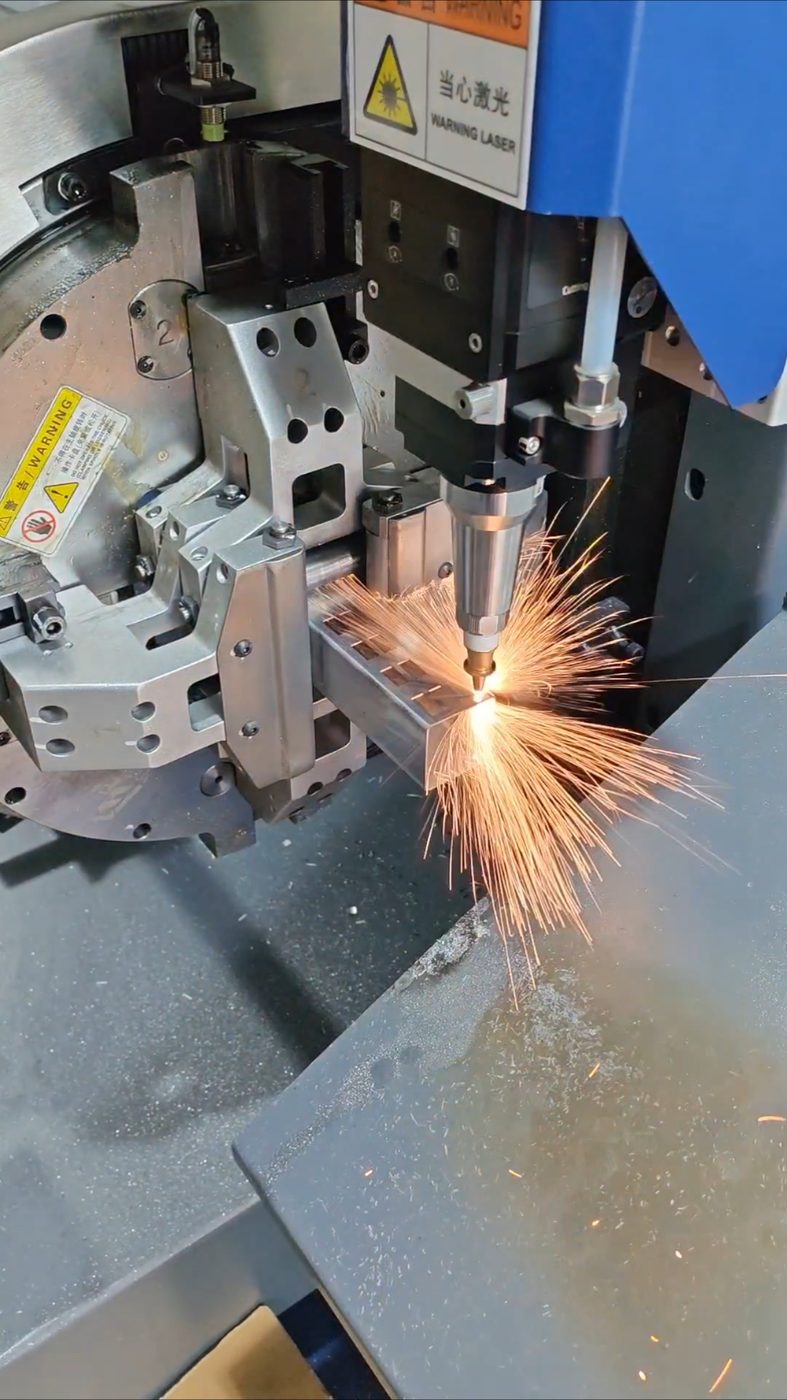
From raw tube and sheet to finished, zinc-plated assemblies — laser cutting, robotic welding, bending, stamping and CNC machining, all in our own 20-year-old workshop.
Send Your DrawingRimzer is a full-service metal fabricator. Hand us a print and receive a finished part — cut, formed, welded, machined, plated, inspected and packed — without coordinating five different suppliers. Below is what each process in our shop does for your part, followed by the numbers procurement teams actually ask for: tolerances, materials, finishes, lead times and the design rules that keep a part cheap to make.
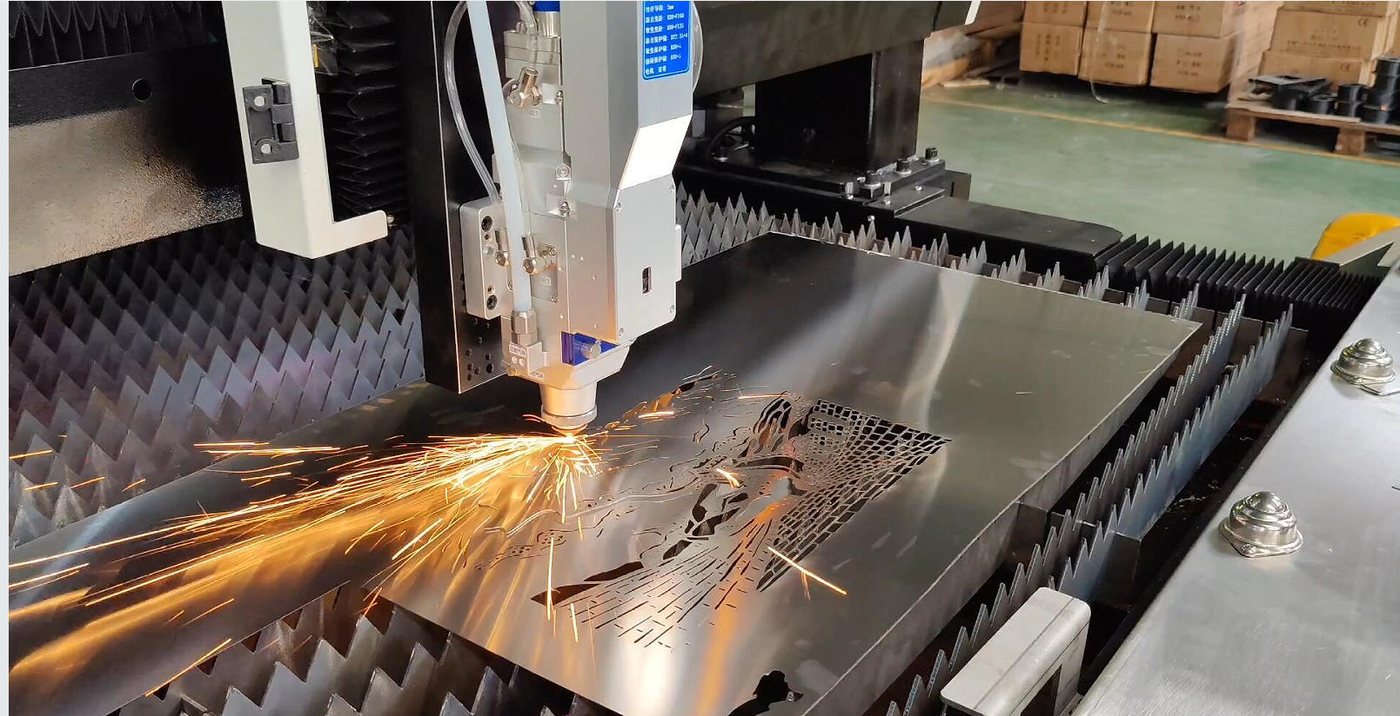
Our CNC laser cuts round, square and rectangular tube as well as sheet and plate. Copes, slots, lightening holes and weld-prep cutouts come off the machine burr-light and dimensionally consistent, so downstream welding fixtures see the same part every time.
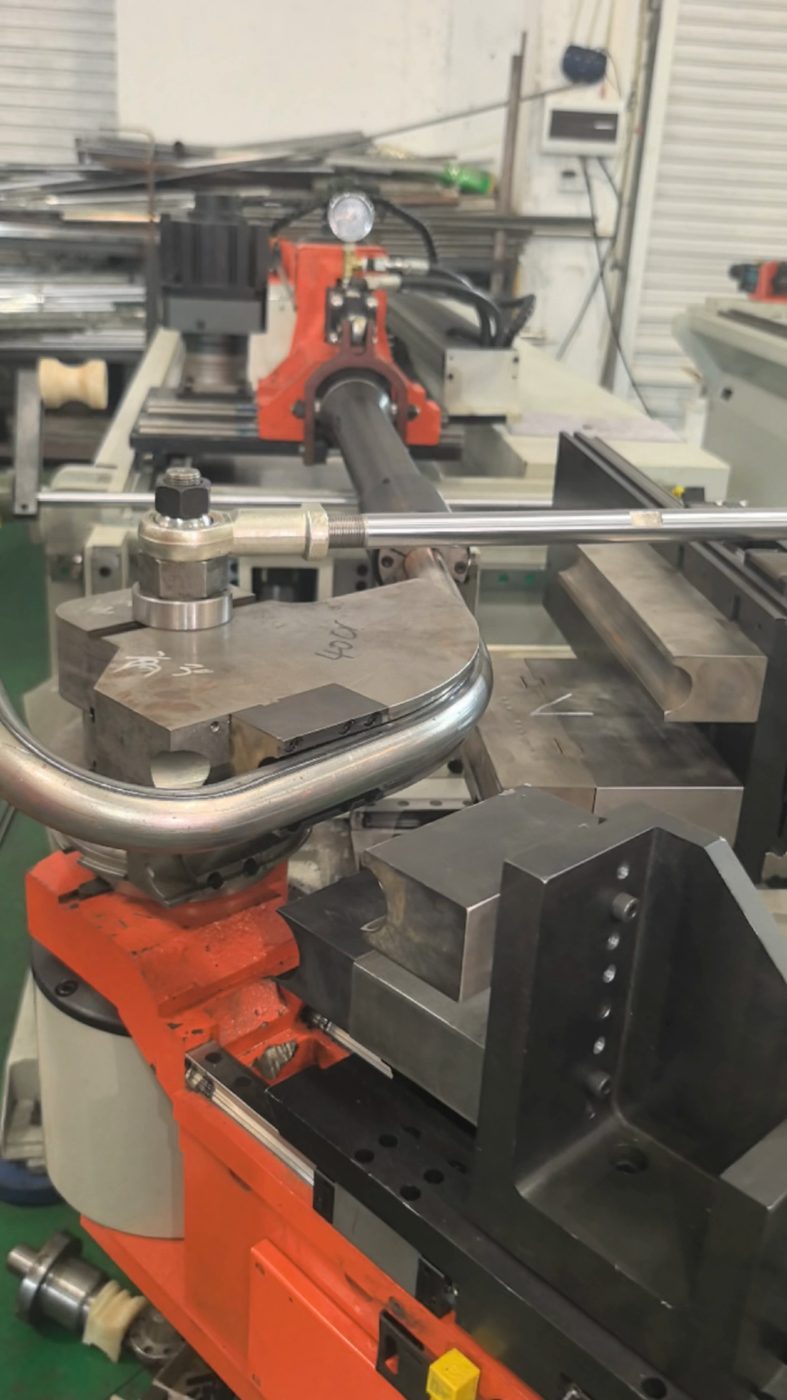
Multi-radius bends in steel, stainless and aluminum tube — handles, hoops, frames and rails. We make and maintain our own bending dies, which means new radii cost you a tooling fee once, not a per-batch premium forever.
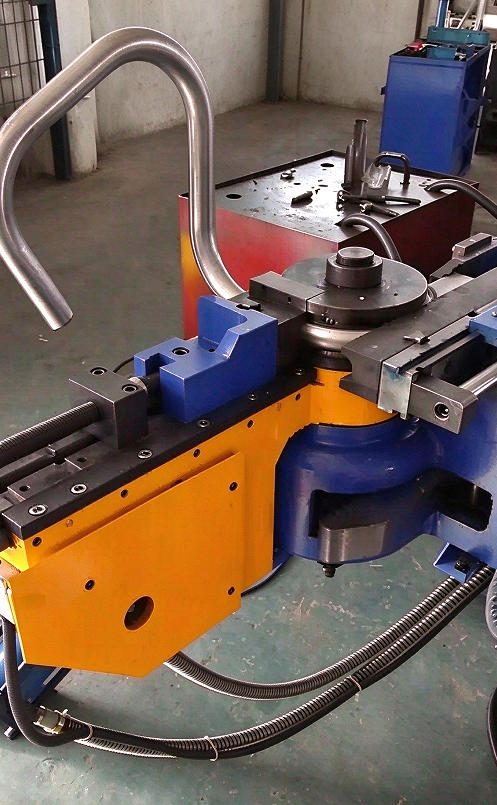
Multiple bending lines run in parallel, so a rush order does not have to displace your routine program. Program data is stored per part number — a reorder six months later bends exactly like the first shipment.
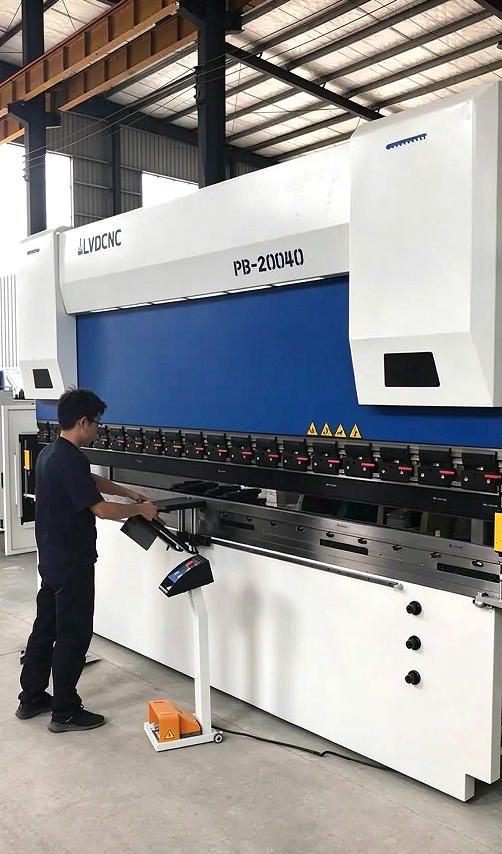
Our CNC press brake handles brackets, panels, channels and enclosures with programmable back-gauge positions. First-article inspection on every setup keeps flange angles inside tolerance from batch one to batch five hundred.
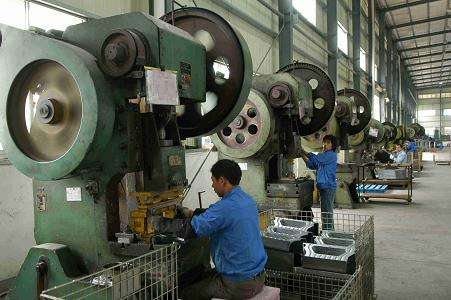
Mechanical presses turn out high-volume small parts — washers, brackets, bin hardware, caster components — at per-piece costs that machining cannot touch. Compound and progressive tooling is designed in-house.
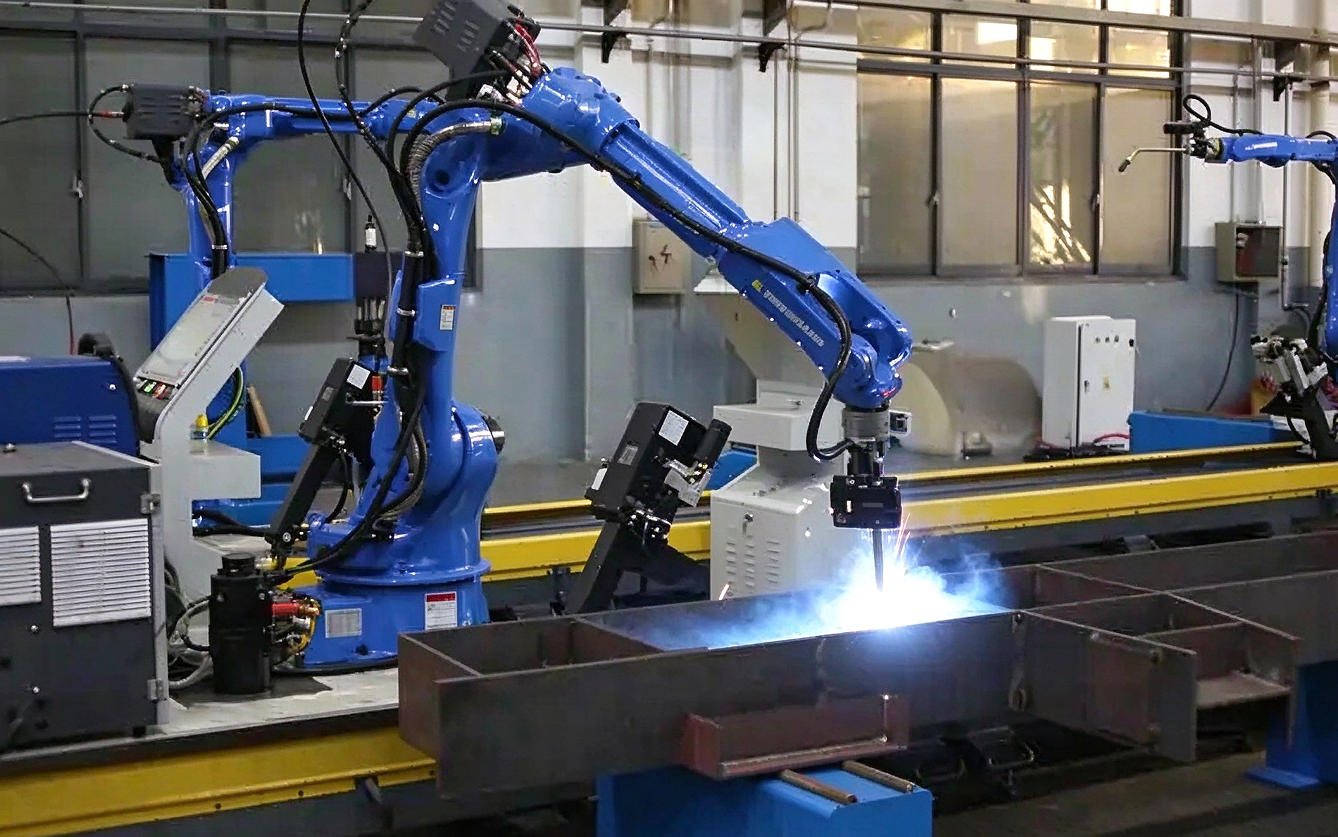
Robotic welding cells deliver repeatable, spatter-controlled seams on frames and assemblies. For a weldment, the robot is only half the story: the fixture decides the outcome. Our weld fixtures and checking fixtures are made and maintained by our own toolroom, many of them by craftsmen with more than 20 years on the bench.
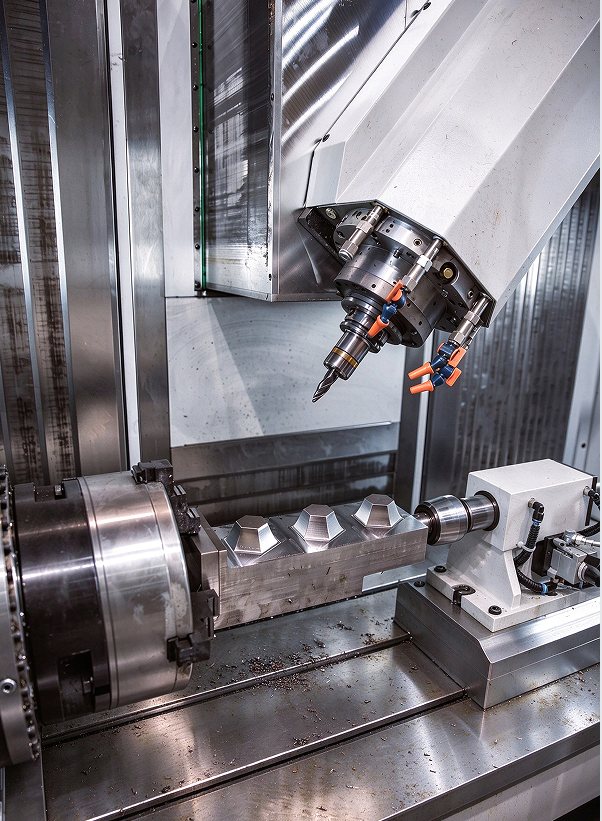
Axles, pins, bushings and turned fittings that must mate with bearings, wheels and molded parts are produced on our precision lathes and CNC turn-mill centers. True position and surface finish here decide whether your assembly runs smooth — this is where our two decades of experience show up most.
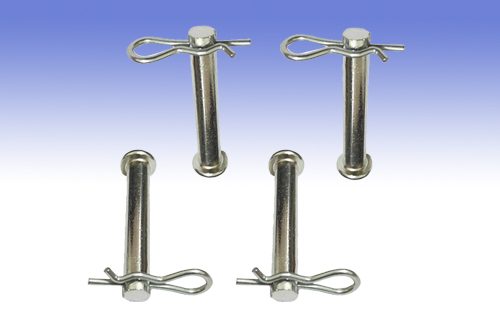
Pins, clips, couplers and fasteners — the parts that look simple are the ones that punish loose process control. Machined, heat-treated where required, zinc-plated and bag-counted, they arrive ready for your assembly line.
These are the numbers we hold in daily production, not a best-case laboratory figure. If your print is tighter than this, tell us before we quote — sometimes we can, and sometimes the honest answer is no.
| Process | Working range | Typical tolerance | Notes |
|---|---|---|---|
| Laser cutting — sheet | 0.5–12 mm carbon steel; 0.5–6 mm stainless | ±0.1–0.2 mm | Kerf approx. 0.2 mm, cut edge Ra 3.2 or better |
| Laser cutting — tube | OD 20–220 mm, wall 1–8 mm | ±0.15 mm | Holes, slots and copes cut in a single setup |
| CNC tube bending | OD 16–76 mm, wall 1.2–4 mm | ±0.5° per bend; ±0.5 mm position | Mandrel bending for centreline radius under 2×OD |
| Press brake | Up to 200 t / 4000 mm; 0.5–8 mm sheet | ±0.3 mm flange; ±0.5° angle | Programmable back gauge, first-article checked |
| Stamping | 0.3–4 mm; presses up to 160 t | ±0.05–0.1 mm | Tooling lead time 15–25 days |
| Robotic MIG welding | Frames up to approx. 2000 × 1200 mm | ±0.5 mm, fixture-held | Repeatable bead profile and penetration |
| CNC turning | Ø5–120 mm, length up to 500 mm | ±0.02 mm; Ra 1.6 | Runout and diameter gauged per batch |
Quote to your own standard or let us propose one. Material certificates come with every shipment.
| Chinese grade | Nearest EN | Nearest ASTM / AISI | Typical use in our shop |
|---|---|---|---|
| Q235B | S235JR | A36 (approx.) | General frames, brackets, bin hardware |
| Q345B | S355JR | A572 Gr. 50 | Load-bearing frames and supports |
| 20# | C22 / 1.0402 | 1020 | Tube, bent parts, general machined items |
| 45# | C45 / 1.0503 | 1045 | Axles, pins, turned components |
| SPCC | DC01 | 1008 CRS | Sheet-metal brackets, covers, small stampings |
| 304 | 1.4301 | S30400 | Stainless frames, food-adjacent parts |
| 316L | 1.4404 | S31603 | Marine, chemical and washdown environments |
| 6061-T6 | EN AW-6061 | 6061-T6 | Lightweight brackets and covers |
Grades are shown as nearest equivalents, not as certified substitutions. Where a standard matters — pressure, structural, food contact — tell us the exact specification and we will quote to it, with the mill certificate matched to that standard.
Electro-galvanizing, hot-dip galvanizing, powder coating and e-coating run through partners we audit annually, all within a short drive of the factory. Taizhou's plating industry is mature: stable bath chemistry, batch-to-batch coating weight control, and wastewater treatment that meets national discharge standards — so the environmental cost is controlled rather than pushed onto someone else's river.
| Finish | Typical thickness | Salt spray (indicative) | Best for |
|---|---|---|---|
| Electro-galvanized, clear / blue | 5–12 µm | 48–96 h | Bin hardware, indoor/outdoor brackets |
| Electro-galvanized, yellow | 8–15 µm | 72–120 h | Higher-humidity service |
| Hot-dip galvanized | 45–85 µm | 200–500 h | Outdoor structures, scaffold parts |
| Powder coating | 60–90 µm | 300–500 h with pretreatment | Visible parts, colour matching |
| E-coating | 15–25 µm | 240–400 h | Complex shapes, sharp edges |
| Zinc-nickel (on request) | 8–15 µm | 500 h+ | Automotive-grade corrosion demand |
Salt-spray figures are indicative ranges for the coating class, not a guarantee for your geometry. If corrosion life is the deciding factor, send us the service environment and we will specify the finish rather than let you guess.
Most cost in fabricated parts is decided at the drawing stage. These are the rules our engineers apply every day — applying them before you send the RFQ usually saves more than any negotiation afterwards.
| Feature | Rule of thumb | Why it matters |
|---|---|---|
| Minimum bend radius | 1× thickness (mild steel); 1.5× across the rolling grain | Tighter radii crack or need annealing |
| Hole-to-bend distance | ≥ 2.5× thickness + bend radius | Closer holes deform into the bend zone |
| Punched hole diameter | ≥ 1× thickness (laser can go to 0.5×) | Small punched holes break punches |
| Tube bend radius | ≥ 2×OD without mandrel; ≥ 1.5×OD with mandrel | Prevents wrinkling and wall thinning |
| Weld access | 25 mm clearance at 45° around every seam | Robot and operator both need torch angle |
| Tolerance stacking | Tolerance only the functional dimensions | Over-tolerancing adds cost, not quality |
| Edge finish callout | State deburr / countersink side explicitly | Ambiguity becomes rework |
Working days from drawing approval and deposit. Existing customers will recognise these numbers — we quote them rather than promise them.
| Item | Sample | Production |
|---|---|---|
| Laser-cut flat parts | 5–7 days | 10–15 days |
| Bent tube / welded frame | 7–10 days | 20–30 days |
| Stamped part with new tooling | Tooling 15–25 days | 25–40 days total |
| Turned parts (axles, pins) | 5–7 days | 15–25 days |
| Galvanized bin hardware | From stock where available | 20–30 days |
| Standard casters | 3–5 days | 15–25 days |
Plan around the Chinese New Year: production effectively stops for 2–3 weeks in late January or February, and the two weeks before it are the busiest of the year. Orders confirmed by early December ship comfortably; orders placed in mid-January rarely do.
Incoming material certificates, first-article inspection on every setup, in-process spot checks and final AQL sampling before packing — plus dedicated checking fixtures for critical geometry. Two examples from our daily routine:
Welded frame verified in its dedicated inspection fixture.
Random pull-testing of handles straight off the packing line.
The faster this list is complete, the faster we can quote a number you can actually plan around. Missing items usually cost a round of emails.
Send what you have, even if the list is half empty. A photo of the part in service plus the critical dimensions is often enough for us to quote and suggest a better way to make it.
Wheeled waste containers and material handling • caster and wheel assemblies • scaffolding and access equipment • appliance and furniture frames • agricultural implements • OEM brackets and machined fittings.
Tell us what the part has to do — we will propose the fastest, cheapest way to make it well.
Request a Quote